Start With The Right Board For The Job
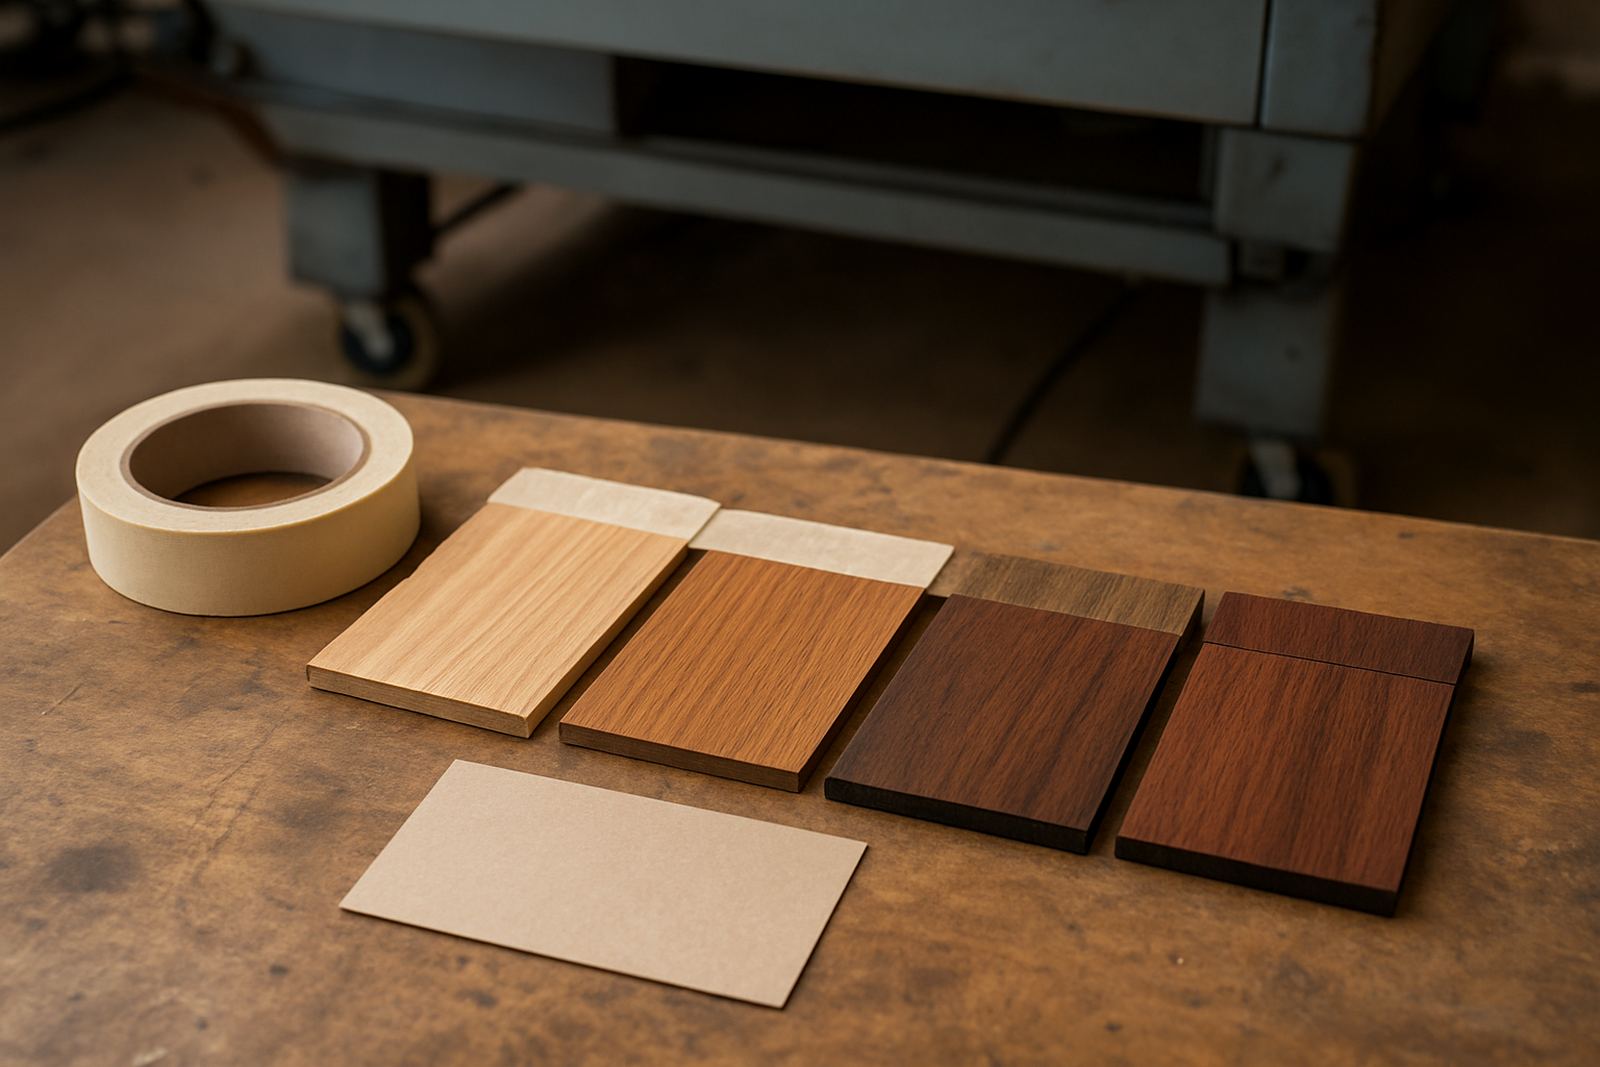
Plywood, MDF and solid timber all behave differently under a CO2 laser. Plywood can cut very neatly, but glue lines and internal voids may leave dark spots or small breakouts. MDF is more consistent and gives smoother edges, although the dust load is heavier and needs proper extraction. Timber is the most variable because grain direction, knots and moisture content all affect the finish.
If you are cutting for signage, packaging, décor or component parts, choose material that suits the end use. For example, 3 mm MDF is often easier for detailed work than rough timber, while good quality birch plywood usually gives cleaner results than low grade multi-ply with gaps. A board that looks cheaper at the supplier can cost more once you factor in rejects and rework.
- Check the board for warping before loading it onto the bed.
- Look for open edges, knots, splits and patchy glue lines.
- Match the sheet thickness to the detail level you need.
Thickness, Moisture And Storage Make A Big Difference
Material thickness affects how much energy the beam must put in to complete the cut. A 3 mm sheet will behave very differently from 9 mm stock, even if both are called plywood. As thickness increases, you usually need slower speeds, more passes or a different cut strategy to keep the edge clean.
Moisture content matters just as much. In Johannesburg winters, dry indoor storage often helps with stable cutting, but in Durban or other coastal areas boards can pick up moisture quickly from humidity. Damp material can scorch more easily and may not cut evenly right through. Timber stored next to an open roller door, or under a roof that leaks a bit, can shift size and curl at the corners.
- Store sheets flat on a level surface, off the floor.
- Keep them away from direct sunlight and damp walls.
- Let newly delivered stock acclimatise before cutting.
Prepare The Sheet Before You Press Start
Good preparation saves time later. Remove dust, stickers and packing debris because any loose dirt can mark the underside of the sheet and interfere with airflow. If the sheet has a protective film, test a small corner first to confirm whether it is safe to leave on during cutting. Some films melt and leave sticky residue, so it is better to know upfront.
Also check your support surface. A sheet that sags between slats can produce tapering on the cut edge and slightly rough bottoms. Flat support with enough clearance for fumes gives better consistency, especially on larger jobs. If the bed is uneven, you may see small focus variations across the sheet and that shows up in the final edge.
- Clean the top and underside of the material.
- Confirm the sheet lies flat with no bounce.
- Secure small pieces so they do not shift during the cut.
Set Power, Speed And Focus To Suit The Material
The best settings depend on the exact board, machine condition and lens setup. Start with a small test piece and adjust before running a full sheet. Too much power can char the edges and widen the kerf, while too little power leaves tabs or incomplete cuts. Speed and power work together, so a small change in one setting often means adjusting the other as well.
Focus is another key point. If the beam is not properly focused on the surface or slightly below it, the cut can look uneven from top to bottom. Beam alignment also affects consistency across the bed. On busy sites, a quick focus check before each shift is worth it, especially after lens cleaning, nozzle changes or machine movement. If the machine was relocated recently, recheck the full setup before production starts.
Keep a simple settings log for each material type. Write down thickness, sheet type, success rate and finish quality. That makes repeat jobs faster and helps operators avoid guessing. It also reduces scrap when more than one person is running the machine.
Control Smoke, Flames And Edge Quality
Plywood and MDF produce a lot of smoke, so extraction has a direct impact on cut quality. If fumes sit in the cut path, the edge can discolour and the surface may get a smoky film that is hard to remove. Good airflow also helps prevent flare ups on resin-rich timber and keeps the machine cleaner over time.
For better results, watch the first minute of the cut closely. If you see excessive sparking, flame bursts or heavy brown staining, stop and adjust the settings or check the extraction system. Coastal humidity, worn optics and dirty mirrors can all contribute to a poorer finish. Regular optics cleaning and cooling checks help keep performance stable, and a blocked airflow path can undo everything very quickly.
- Empty or service extraction filters on schedule.
- Inspect lenses and mirrors for dust or residue.
- Check chiller temperature and water flow before long runs.
Run A Simple Quality Check Before Batch Production
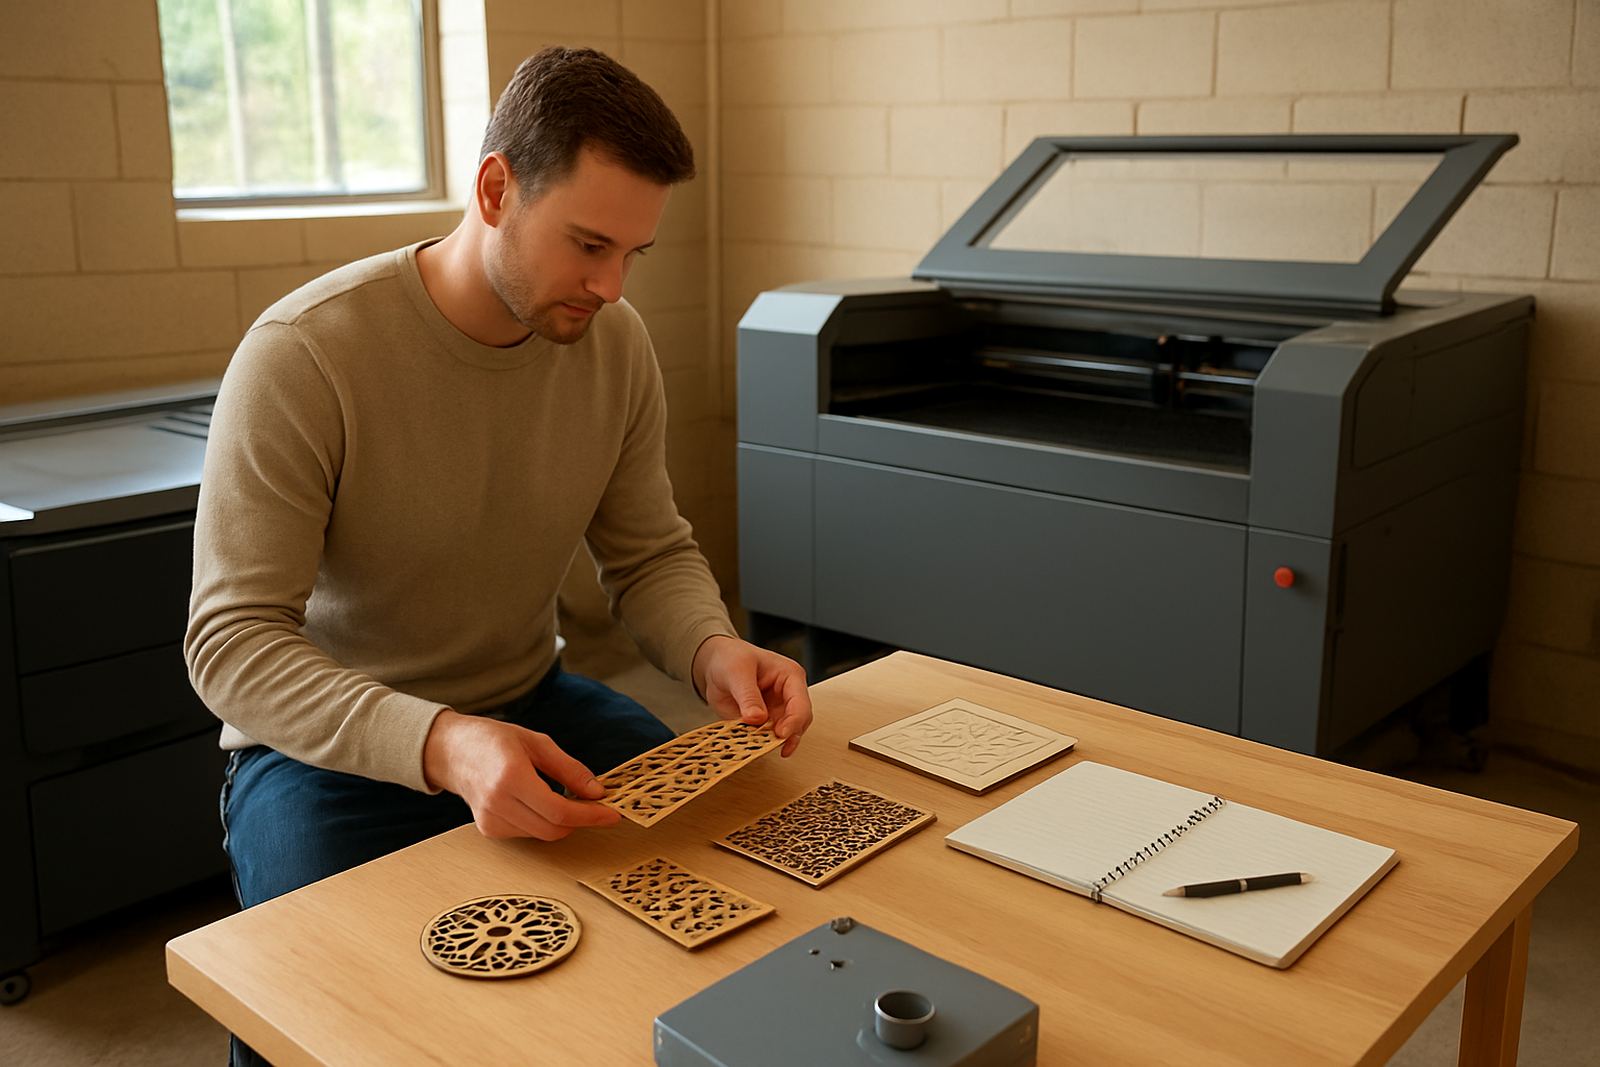
Before you commit to a large run, inspect one finished part carefully. Look at the edge colour, the amount of taper, the amount of smoke staining and whether small internal corners have fully cut through. If the sample is good, use the same settings and material batch for the rest of the job. If it is not, fix the issue before you waste a full sheet stack.
A practical workshop checklist helps operators stay consistent. It also makes handovers easier when more than one person uses the machine. In larger workshops around Sandton, Midrand, Pretoria and the East Rand, this kind of process control can save a lot of time during busy weeks and load-shedding interruptions.
- Confirm material type and thickness.
- Check focus, alignment and extraction.
- Cut a sample and inspect the edge.
- Record the final settings for repeat work.